Background
The life of a vessel under cyclic service is related to the intensity of the alternating stress and the number of cycles it experiences. The fatigue life curves used under ASME VIII-2 to calculate the permitted cycle life of a vessel are based on a large factor of safety compared with actual cycle life curves. VIII-2 fatigue methods calculate an allowable number of operating cycles with a factor of safety. They do not predict the cycle life of the vessel which normally will be larger. [1,2] The equations found in ASME code books rarely provide real stresses that can be used to compute permissible cycle life. Equations for items such as Heads [3], Flanges, nozzles and others are design rules which cannot predict real stresses in any particular location of a vessel. Large factors of safety make their real world use acceptable, but not useful for fatigue calculations. To get stress values for cycle life calculations Finite Element Analysis (FEA) is required. Areas in a FEA either converge to a fixed value, or run away to infinity as the mesh size is reduced. This traces back to the work of Ingles and stress concentration factors [5]. In theory, any area with a sharp corner has stresses that rise to infinity. The FEA error plot is used to determine which areas converge and which do not [4]. Typical areas that do not converge are: toes of nozzle welds; any transition in shell thickness with sharp edges like a 3:1 taper; any sharp change in direction like shell to flat head or shell to flange connections; and areas under bolt heads or other connectors. The reported stresses in these areas are mesh size dependent. There is no mesh size possible that will give accurate stress results [8]. Special methods are used to determine the cycle life in these areas.
The Sample
This cycle life sample shows direct reading of stresses in converged areas, and two methods of determining the correct stress to use for areas that have not converged. ASME provides factors for modifying stresses to allow for surface finish quality and surface and volumetric inspection levels. These factors are multiplied by the stresses to produce a factored stress for a location. The largest factored stress is used to determine the maximum permissible cycle life for this sample vessel.

The simple vessel used for this sample permissible cycle life report.
Downloads:
Converged and Non-converged Areas
The error plot shows areas that are converged and not converged. The mesh has been refined enough that the error has been reduced to less than 5% in areas like the shell and head (Fig 2). Stress can be directly read from the model for these areas. The nozzle welds are discontinuities that produce stress results that are mesh size dependent. These areas need special methods to read the stress results (Report Fig 10).
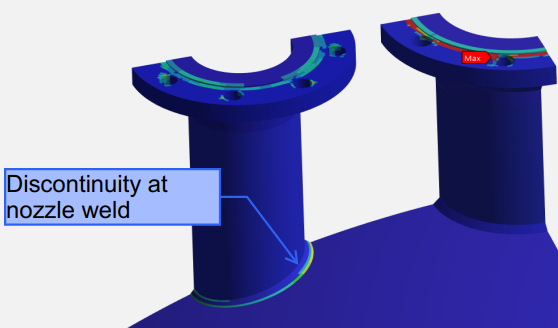
Close up of the discontinuity zone of the nozzle to shell weld. The weld toe is a non-converged discontinuity that produces stress results that are mesh size dependent. It is not possible to directly read the stresses here.
Converged Areas – Direct Stress Reading
The head knuckle is full converged allowing the stress to be directly read – see Fig-9. Other areas on the vessel cannot be directly read.
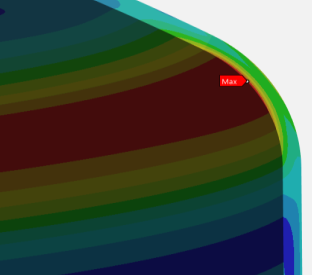
Note that the Kf factor is 1.0 for this location as the stress is base metal.
Non-Converged areas – Linearization
The method of linearization for non-converged areas is covered in ASME VIII-2 section 5.5.3. It is shown in an easier to understand manner in ASME PTB-3-2010 section 5.5.3 [6]. For this sample multiple areas are linearized to provide stresses for areas that are and are not converged. For example Fig 10 (report page 15) shows a stress classification line taken through the toe of a weld to get a converged peak stress even though the toe is not converged. To get a converged result, the mesh has to be refined enough that at least half the elements along the SCL reach an error level less than 5%. This typically takes 5 or more nodes along the line [7]. This location passes this criteria and the SCL can be used.
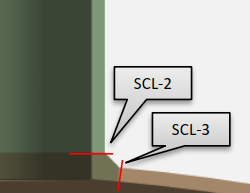
Stress Classification Line through the nozzle weld toe. The error plot (not shown) indicated that half the elements along the line had error less than 5% so the SCL can be used.
Modifying the Measured Stresses – Kf
The stresses measured by the SCL method above is modified according to the surface finish and inspection level of the welded connection. This is ASME factor Kf from table VIII-2 5.11 and 5.12. In this sample job Kf factors range from 1.0 for locations with no welds to 2.5 multiplier for full penetration welds with no volumetric inspection – see page 28 for example. The Kf factor is added on top of a 4.0x surface finish and environment factor that is already built into the fatigue life curves [1].
Calculating the Permitted Cycle Life
For each location, the measured stress is increased by the above Kf factor. The stress is reduced by a further factor of 2 because the fatigue life curves are made for alternating stresses and this pressure vessel’s stresses do not alternate. Also including the temperature correction results in Se – the equivalent stress used to measure the permitted cycle life from ASME’s charts. Each vessel location has had its permissible cycle life calculated. The lowest permissible life governs the design for the whole vessel – in this case SCL 10 at permitted cycles – (Report page 3). This is not the location of the highest stress in the vessel.
What Happened Here?
The largest conceptual block to overcome is that the ASME methods allow us to take average stresses through areas that are not converged (linearization) to obtain an estimated stress and a derived permissible cycle life. Why should this work? Two important reasons:
- The materials used are ductile. Although in theory the stresses rise to infinity at a discontinuity, in practice once they reach the yield point, the material moves and re-distributes the stresses. This happens during the hydro test. These methods will not work for brittle materials like cast iron or glass where the designer must remove the sharp discontinuities.
- The permissible fatigue curves have a large factor of safety. No stress concentration factor was added to the linearized stresses because the curves already have a shape factor of 2.5x [1,2]. However, the stresses were increased depending on the surface condition/inspection level of the location even though a 4x surface factor was already included[1]. Other factors are also included in the curves resulting in an overall 20x factor of safety. These ASME methods are approximate but large safety methods make them practical.
To repeat – we are not calculating the expected cycle life of the pressure vessel using these methods; we are calculating a permissible operating life with a large safety margin.
More Information
[1] Fatigue Design of Process Equipment, ASME Plant Engineering & Maintenance Technical Chapter, March 12, 2009, Chris Hinnant, Paulin Research Group, Houston, TX Presentation (pdf) See pages 20 and 37. [2]PVEng – Origins of the ASME Fatigue Life Curves
[3]PVEng – Discontinuity Stresses in Flange and Dished heads
[4]PVEng – Using the Error Function Results for Areas at Discontinuities
[5] J.E. Gordon, The New Science of Strong Materials or Why You Don’t Fall Through the Floor – Chapter 4 – Cracks and Dislocations. Penguin books 1968, Second Edition 1976. Some new reprints of Mr. Gordon’s books have photos that are poorly scanned and printed so the concepts being discussed are not visible. Try for an original print.
[6] PTB-3-2013 “ASME Section VIII – Division 2 Example Problem Manual” Page 5-32 to 5-38. This book is highly recommended as it provides illustrated use of the rules provided in ASME VIII-2. ASME
[7] PVEng – in development, not released yet.
[8] PVEng – Mesh Refinement Using the Error Function Results for Areas Near Discontinuities.
File: PVE-5522 & 6160, Last Updated: Oct 25, 2012, By: LRB/CBM/MAH
